Why end-of-shift checks matter on sealing lines
On an induction sealing line, small problems build up quickly if they are left until the next shift. A loose guide, a dirty cooling path or a liner mismatch can turn into rejects, stoppages and wasted product. A simple operator checklist at shutdown gives the line a proper close-out, and it helps the next team start clean.
In food, pharma and chemical packing, the seal is part of the product control chain. If a cap seal is damaged, or the cap was not seated correctly, the pack may leave the line looking fine but fail later in transit or storage. That is a costly problem for any plant, especially where deliveries go across KwaZulu-Natal and into inland routes with long travel times.
Start with the seal head and product path
Before the line is switched off, operators should check the seal head area, the cap path and the immediate work zone. This is where dust, bottle splash and foil fragments often collect. If these are not cleared daily, they can affect heat transfer and cause inconsistent sealing the following day.
- Remove loose foil pieces and product residue from the sealing area.
- Check that the capper and conveyor are free of obstructions.
- Look for worn guides, shifted bottles or damaged rollers.
- Confirm that no bottles are stuck under the head or trapped on the belt.
A quick visual inspection takes minutes, but it can prevent an hour of troubleshooting in the morning. It also helps operators spot early wear before it turns into a breakdown. A small rattle today is often a sign of a bigger issue tomorrow.
Check liner condition and cap fit before changeover
Liner quality and fit matter just as much at shutdown as they do at startup. If the wrong liner was used during the shift, or if cap torque drifted, the seal may look fine but fail under transport, vibration or storage heat. Shutdown is the best time to record this and pass it on to the next operator.
- Confirm the correct liner type was used for the bottle and closure.
- Check for scorched, wrinkled or partially bonded liners.
- Note any caps that felt loose, cross-threaded or hard to apply.
- Separate rejected product clearly so it does not return to the line by mistake.
For plants in Jacobs or Prospecton, coastal humidity can also affect packaging during warm afternoons and overnight storage. A liner that performs well at 08:00 may behave differently by 16:00 if the store room is not controlled. That is why operator feedback matters, not just lab results.
Clean around belts, sensors and electrical covers
Many shutdown faults come from dirt rather than major mechanical failure. Adhesive build-up, powdered product and moisture can gather around sensors, belts and covers. If that build-up is left overnight, it attracts more dirt and can interfere with detection or movement when the line starts again.
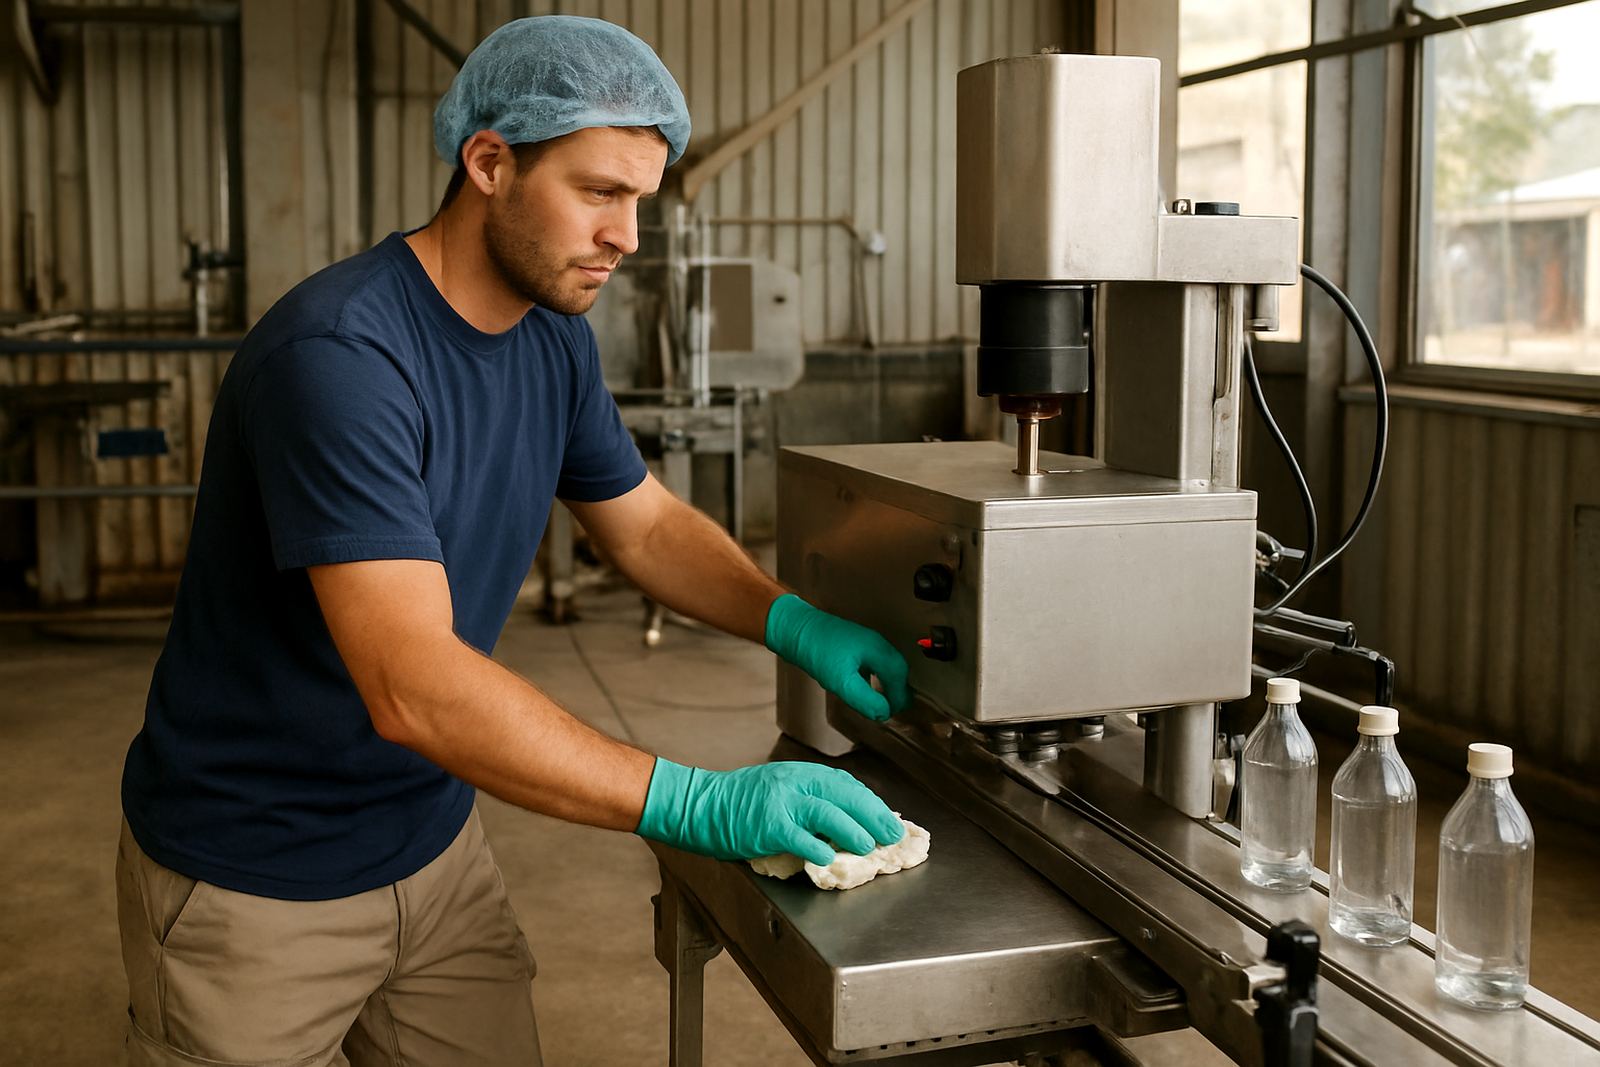
Operators should follow site cleaning rules and only use approved methods for the equipment. Water, cloths and air lines must be used carefully, especially near electrical covers and control panels. In some Durban factories, a quick cleanup after a humid shift is essential because moisture plus dust can form a sticky layer around moving parts.
Good practice at shutdown includes checking that:
- All guards are back in place.
- Sensors are clean and unobstructed.
- Belts are clear of product spill and broken caps.
- No cleaning tools are left on the machine.
Record faults while they are fresh
A proper shutdown is not complete until the operator records what happened during the shift. The person who ran the line knows which bottle size started slipping, when the seal head sounded different, and whether the line slowed after a cap feed issue. That detail is valuable to the technician and the next shift.
Keep the note short but specific. Include the time, the product run, the fault, and what was done to get the line running again. If the line was stopped because of load-shedding or a power dip, write that down too. On return to power, equipment may need a careful restart and validation before full production resumes.
A useful shutdown note can include:
- Product name and bottle size.
- Time the issue started.
- Fault symptoms such as weak seals, jammed caps or alarm lights.
- Action taken by the operator.
- Any follow-up needed for maintenance or quality.
Protect the line for the next shift or overnight stop
Some lines restart a few hours later, while others sit overnight or over a weekend. The shutdown routine should match that reality. If a line is going idle for longer, operators need to secure consumables, isolate power where required, and make sure the area is left safe and tidy.
For plants in Pinetown, Pietermaritzburg or Richards Bay, this becomes even more important when shifts overlap with municipal work, humidity or unstable supply conditions. If a plant expects a power interruption, the team should know how to park the line safely and what checks to make before the next start-up. It saves time and helps avoid damaged liners, misfeeds or false alarms.
Before the line is handed over, make sure that:
- Product in the hopper or feed area is handled according to site rules.
- Loose caps and liners are stored properly.
- Power isolation steps are followed if the line will be idle.
- The work area is left dry, safe and clear for the next crew.
A Durban example that shows the value of routine
At a busy packaging site in Jacobs, a team started using a simple shutdown sheet after repeated morning faults on an induction cap sealer. The issue was not the machine itself. It was a mix of liner dust, cap feed misalignment and a missed note from the previous shift. Once operators began clearing the sealing area, checking cap fit and logging the exact fault before handover, the number of repeat stops dropped quickly.
The result was not dramatic, just practical. Less rework, fewer rejected packs and a calmer start to the next shift. That is usually what a good shutdown checklist delivers. It helps the line stay predictable, even when production pressure is high and the factory is working around transport deadlines or power interruptions.
For supervisors, the checklist also gives a better picture of how the equipment is behaving across the week. That makes it easier to plan preventive maintenance, spare parts and operator training before the line starts giving trouble.
Build the checklist into the shift handover
The best shutdown routines are not complicated. They are short enough for operators to use every day and clear enough for supervisors to check without delay. The point is consistency. If the same steps are followed at the end of each shift, patterns show up early and faults are easier to trace.
A practical shutdown checklist should sit with the handover notes, the cleaning schedule and the maintenance log. It should cover the sealing area, liner condition, cleaning, fault reporting and safe isolation. With that in place, the line is easier to trust and easier to maintain, which matters in any plant that is packing sealed containers for the South African market.
End-of-shift discipline is not extra admin. It is part of protecting the equipment, the product and the people who start the line again tomorrow.