Why cap torque changes the seal outcome
Induction sealing depends on the cap closing the liner evenly against the container finish before heat is applied. If the cap is under-torqued, the liner can sit crooked or leave gaps. If it is over-torqued, the liner may distort, split or stress the neck of the bottle, especially on light PET or thin-walled containers.
In practice, the seal is only as consistent as the closure applied on the line. That is why cap torque should be treated as part of the sealing process, not as a separate bottle filling step. On food, pharma and chemical packs, a small change in torque can mean a leaked carton, a failed tamper check, or a return from the customer.
What too little or too much torque looks like on the line
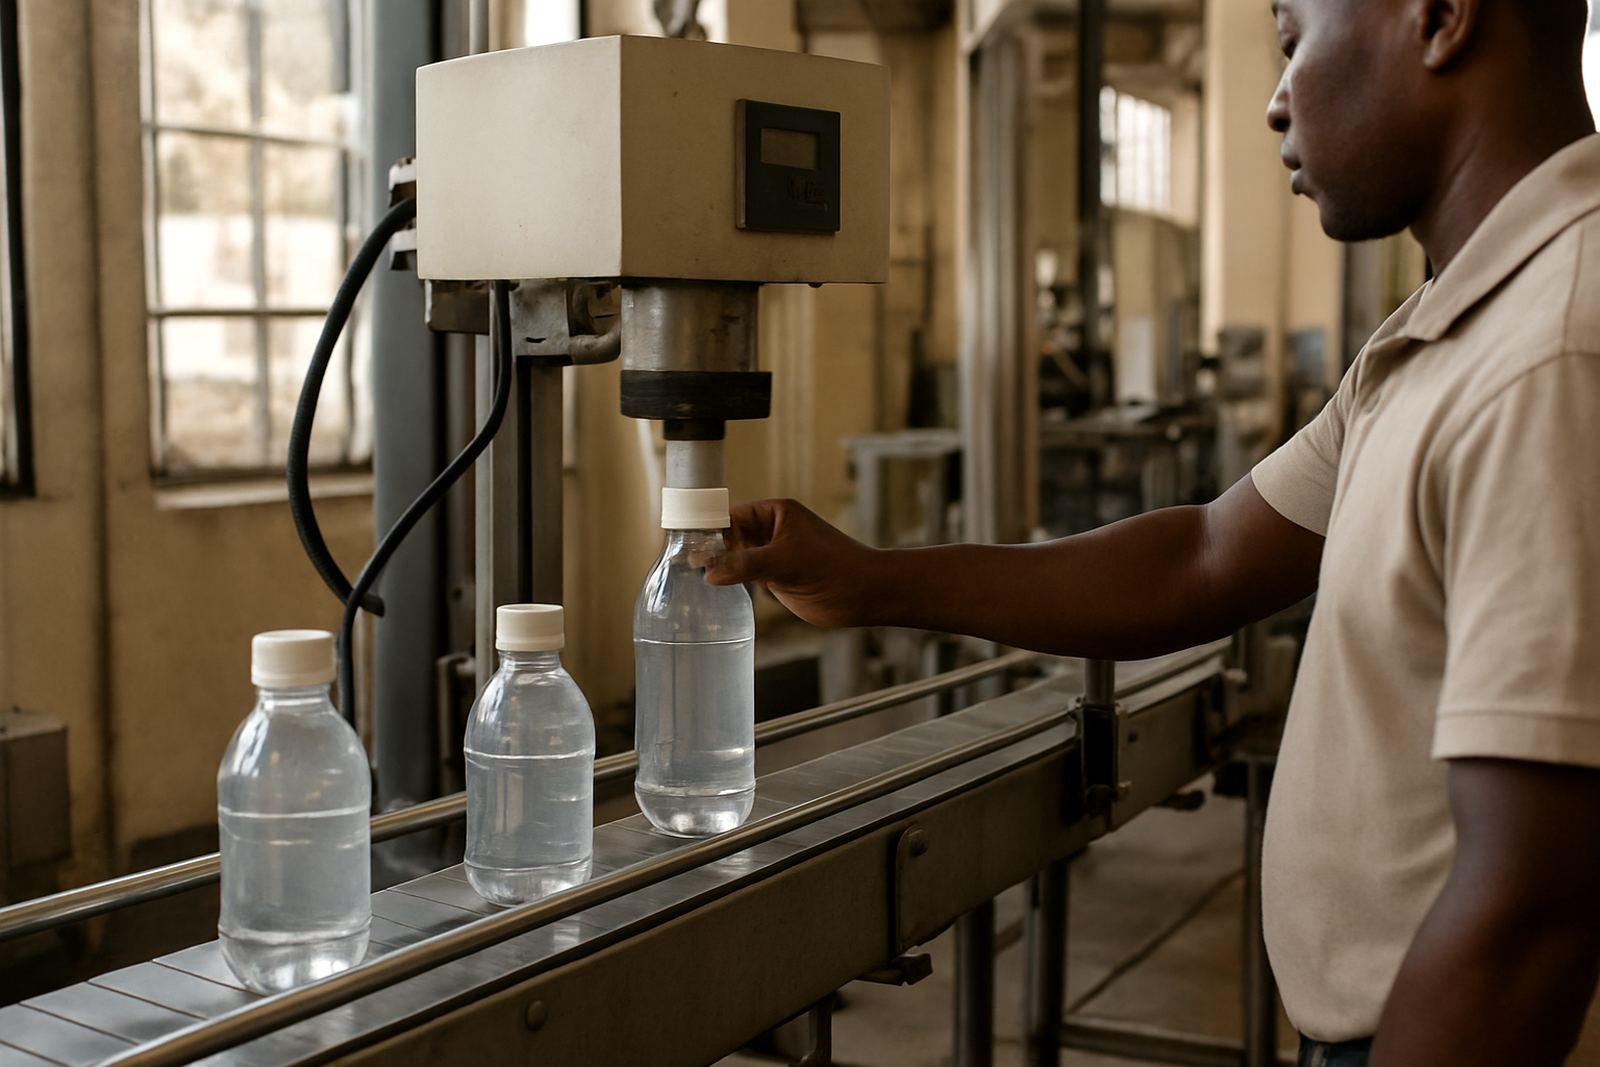
Most sealing faults start before the induction head even comes into play. Operators may see product creep at the thread, caps backing off after handling, or foil liners that show uneven compression. A cap that is too loose can rock during conveyor movement. A cap that is too tight can give a false sense of security because it feels secure but the liner has been crushed unevenly.
- Loose caps can cause poor liner contact and patchy sealing
- Over-tight caps can deform the container shoulder or neck finish
- Torque drift often shows up after changeovers or cap supplier changes
- Warm rooms and humid coastal conditions can affect closure feel during shifts
At a Durban Jacobs site, we often see this after a line has been speeded up for a big batch run. The seal head is not always the problem. Sometimes the capper setting needs attention, or the cap feed is delivering closures inconsistently.
How to check cap torque without slowing production
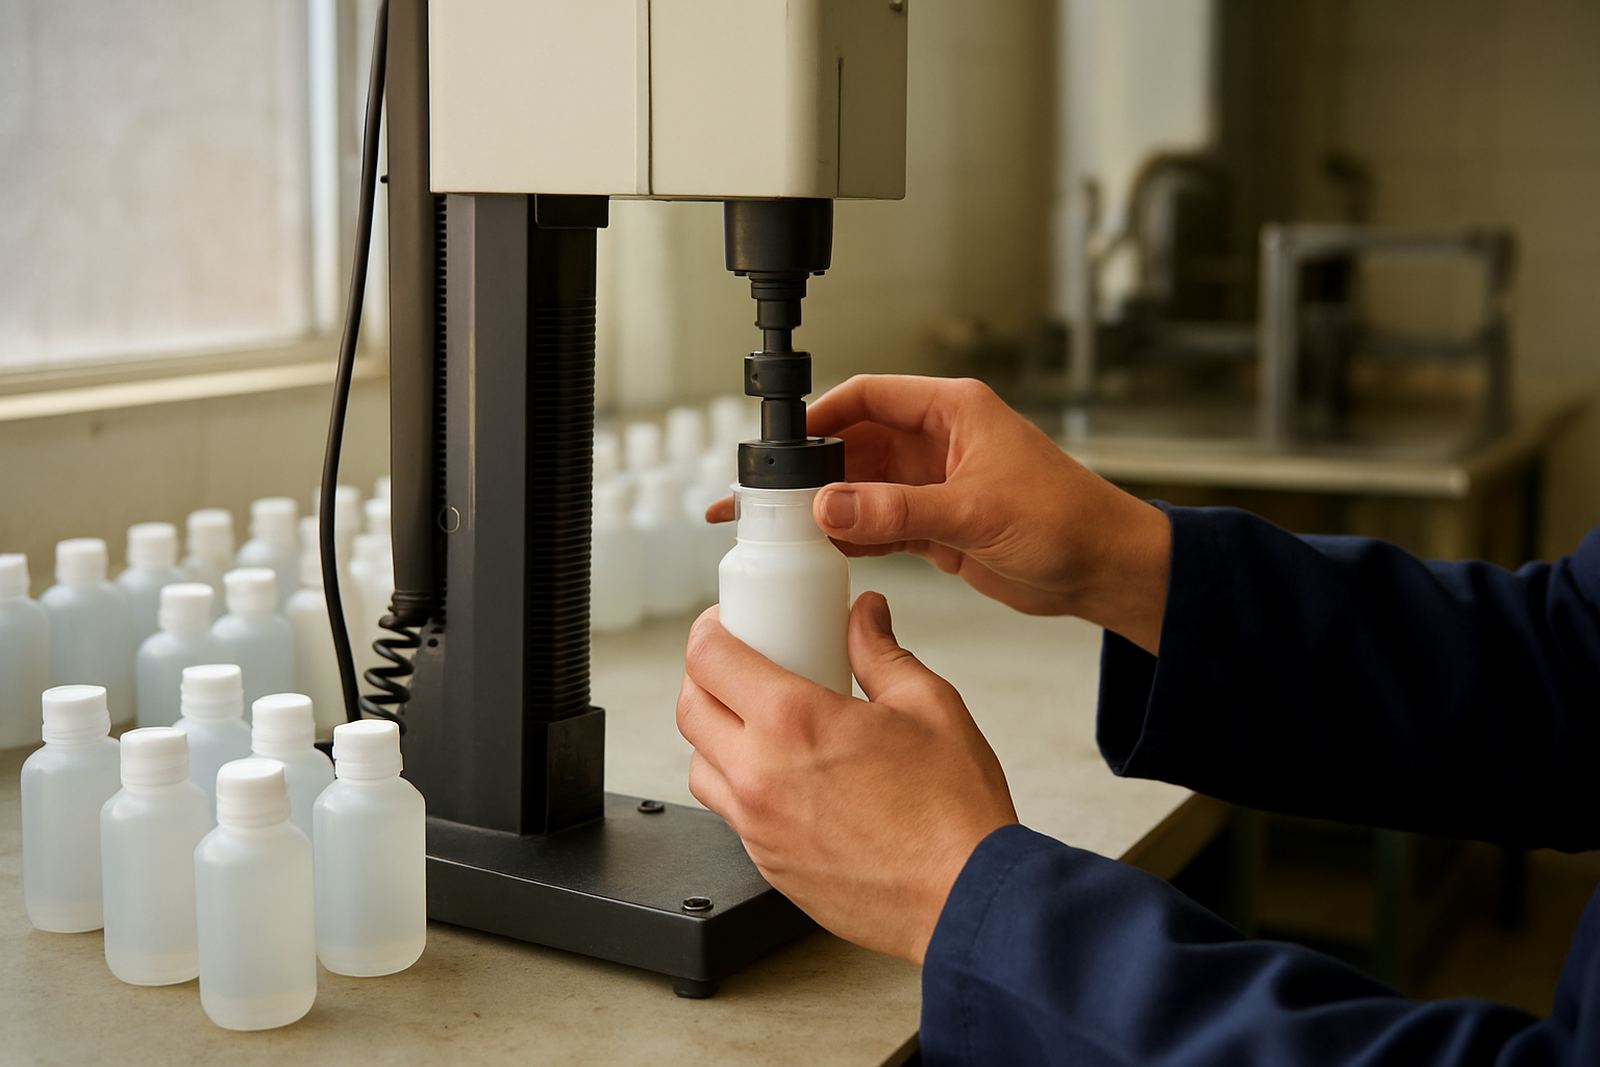
The best method is to set a target torque range and check it at the start of each shift, after changeovers, and when a new liner batch is loaded. Use a calibrated torque tool and test at least a few containers from the first run, then repeat checks once the line has stabilised. Record the results so the operator, supervisor and maintenance team can see trends over time.
Keep the method simple and repeatable. Measure the cap on the same container type, with the same product fill level, and ideally at the same temperature. A container filled hot may behave differently from one filled at room temperature, so a reading taken too early can mislead the team.
- Check torque after any capper adjustment
- Check again after a liner or cap supplier change
- Check during the shift if rejects start rising
- Keep a signed log with time, batch and operator name
Matching torque to the container and liner
There is no single torque setting that suits every pack. Glass jars, HDPE bottles and PET containers all react differently. Some products need a firm hand to keep a heavy cap from loosening in transport. Others need a lighter touch to protect the neck finish and still allow the liner to seal properly under induction.
Foil liners also matter. A liner that is too thick, too thin, or not suited to the neck profile can make the cap feel wrong even when the torque reading looks acceptable. That is why liner matching should be done with the actual closure, bottle and product together, not in isolation.
Common reasons torque drifts during a shift
Torque is often stable in the morning and then starts to wander later in the day. The causes are usually practical rather than mysterious. Small changes in cap feed, worn capping heads, product spillage on the neck, or a slight change in bottle finish can all affect the reading. On a hot day in Richards Bay or during load-shedding recovery, line speed and operator attention can also shift the results.
- Worn or dirty chuck parts
- Incorrect cap height before tightening
- Product on the bottle thread or sealing land
- Different cap batches from the supplier
- Temperature changes in the filling room
Preventive maintenance helps here. Clean, inspect and test the capping section before it starts producing reject after reject. A short stop for adjustment is cheaper than a pallet of returns.
A practical Durban example for better consistency
A small pack line in Jacobs may run detergent on the morning shift and a chemical cleaner later in the day. If the same cap setting is used for both, the second product can show a different torque feel because of residue, bottle movement and operator timing. Once the team set a fixed torque check, cleaned the necks more carefully, and logged the results, seal failures dropped and the induction head had less rework to deal with.
The point is simple. Good sealing starts with a cap that is tight enough to hold steady, but not so tight that it damages the pack. When torque is checked properly, the induction seal does its job more reliably, and the line runs with fewer surprises.