Start with the neck finish, not the label on the cap
When a cap does not seal properly, the problem is often a mismatch between the bottle neck finish and the sealing head setup. A cap may look correct by eye, but if the thread profile, neck diameter or liner position is off, the induction process will struggle to give a clean, even seal. In Jacobs, Durban and on lines running nationwide, we often find that the bottle supplier changed the neck spec slightly and nobody updated the sealing setup.
The neck finish tells you the opening size, thread style and the depth the cap sits on the bottle. That is the starting point for matching cap sizes. If you are sealing pharmaceuticals, food products or chemicals, the finish must stay consistent from batch to batch or your seal quality will drift. Keep one current sample bottle from every approved pack format and compare new deliveries against it before changeover.
Measure the cap diameter and sealing area correctly
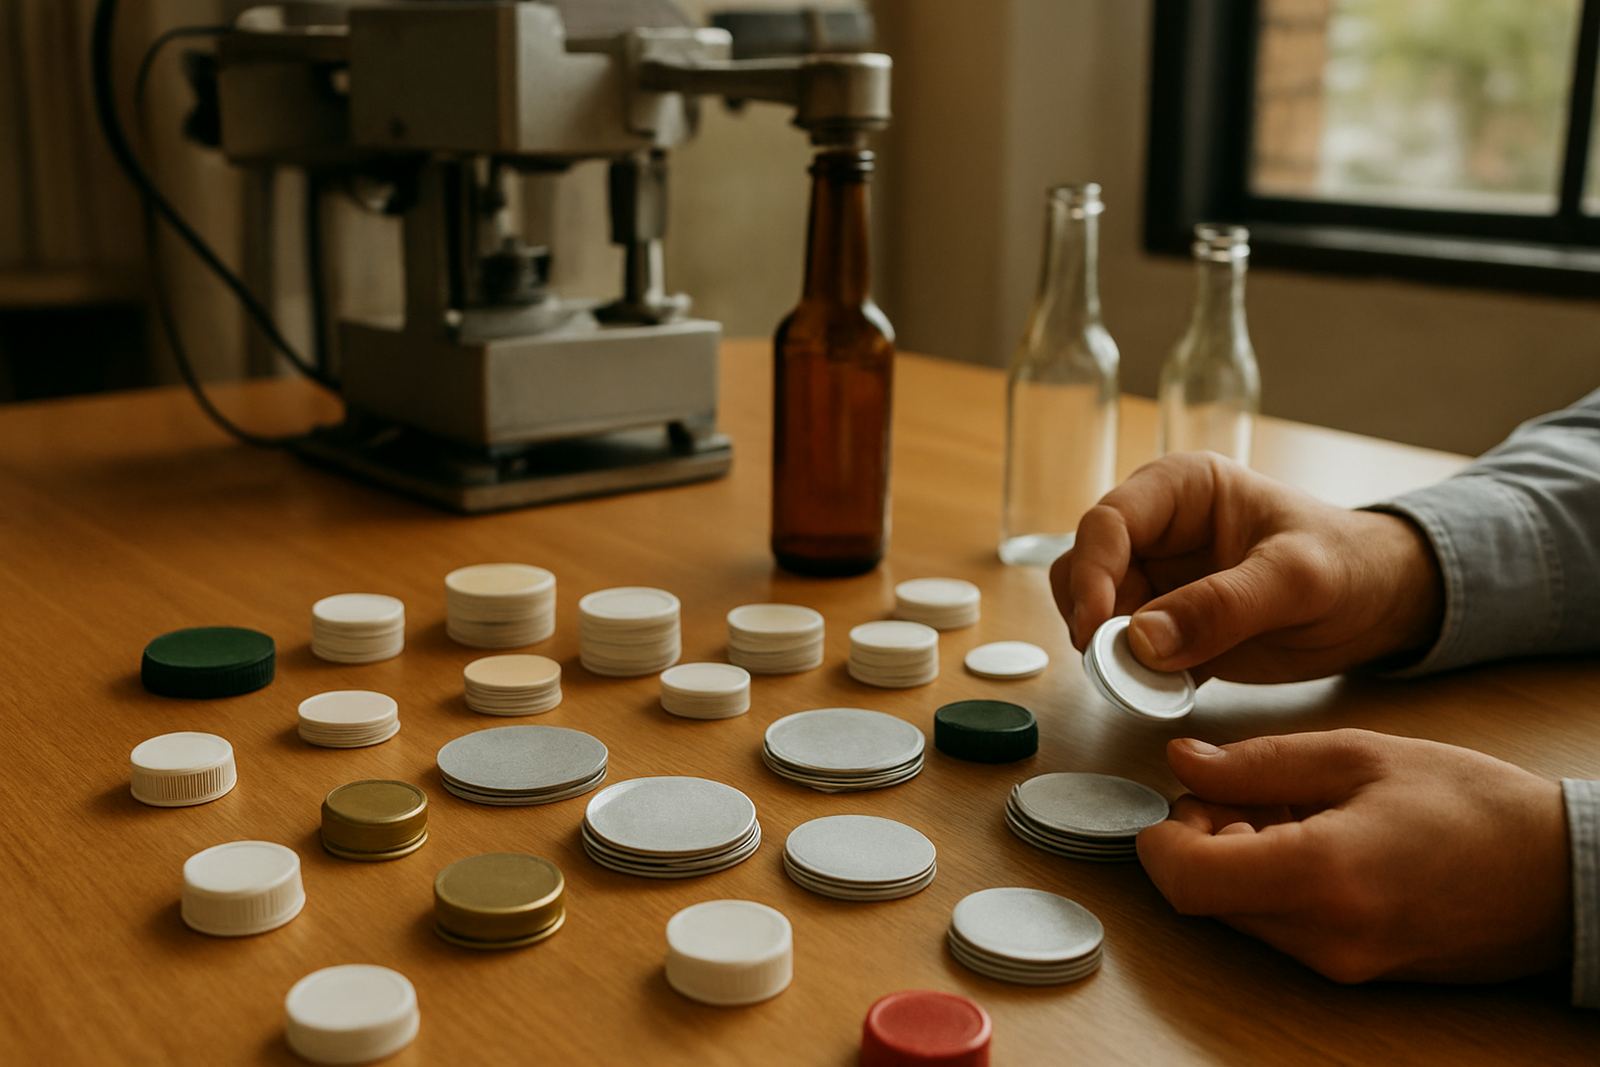
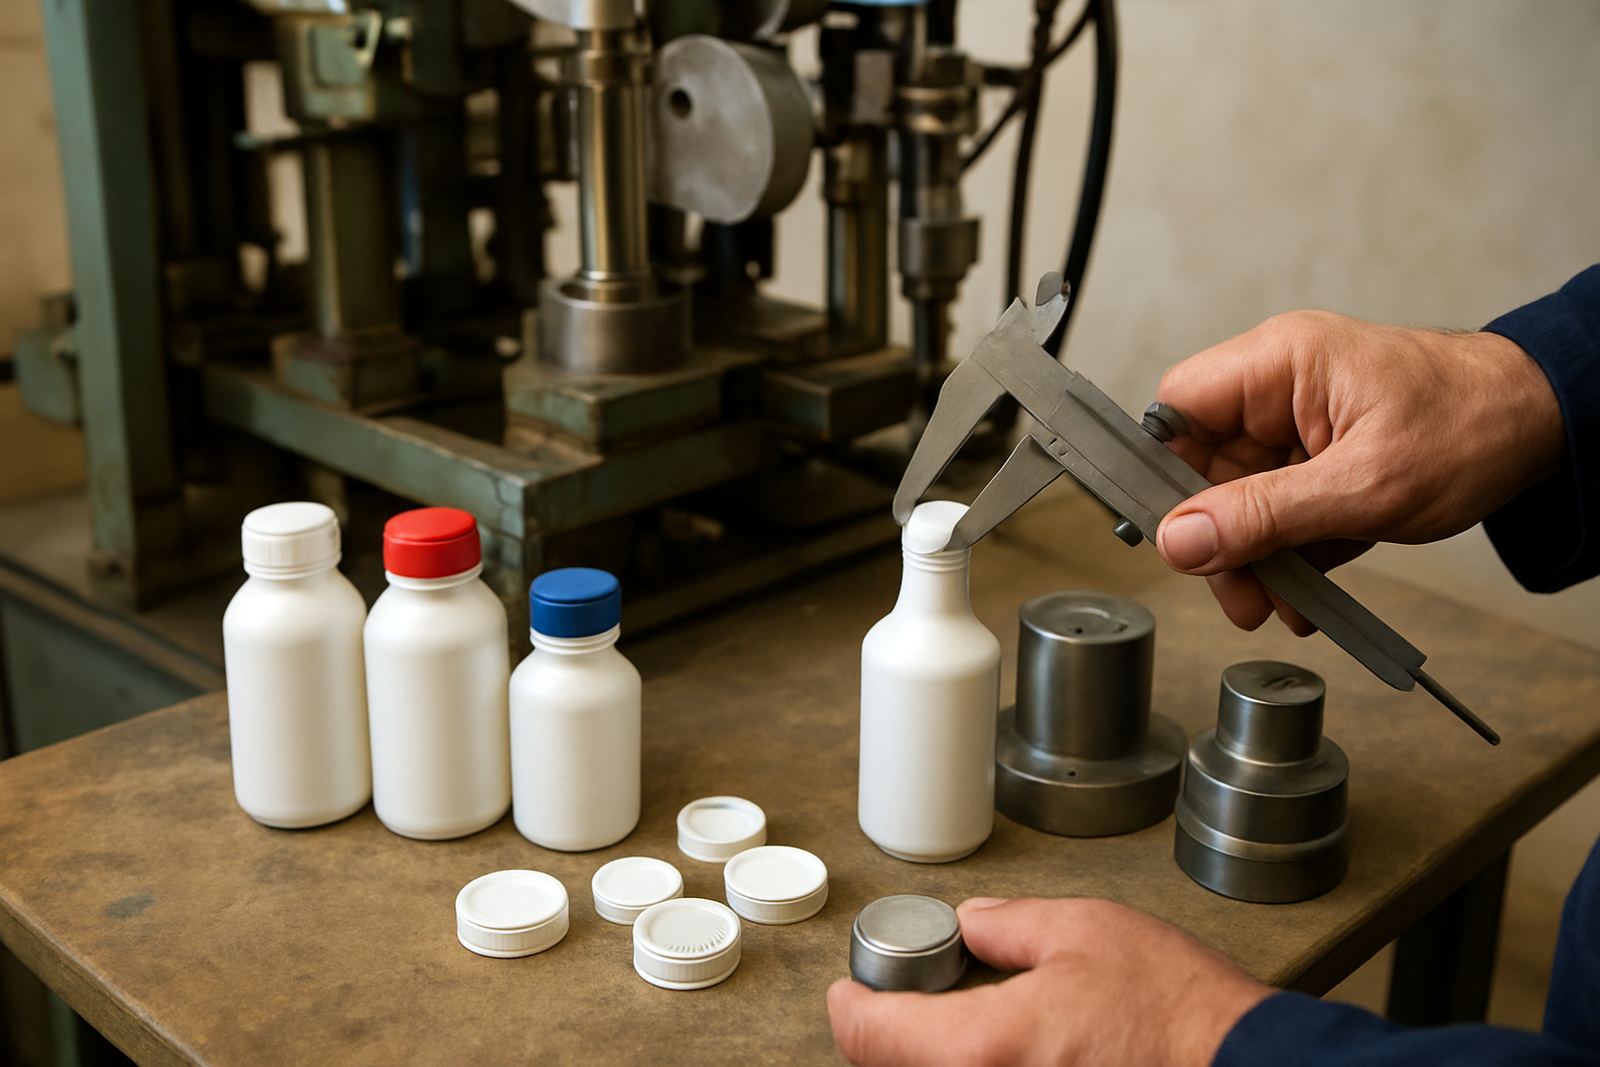
Cap diameter matters, but only when measured properly. For induction sealing you need to know the outside cap size, the inner sealing face and the liner contact area. A cap that is too wide for the sealing head can receive uneven heat, while a cap that is too small may leave part of the foil liner underprocessed. That can lead to leaks, tamper issues or product recalls.
- Measure the cap across the widest point with a calibrated calliper.
- Check the cap height so the head can make full contact during the cycle.
- Confirm the liner sits flat and is centred, not skewed inside the cap.
- Compare the cap size against the bottle neck finish sample, not only the drawing.
If your packaging team is changing cap colours or suppliers, repeat the measurements every time. Small differences of 1 mm or 2 mm can matter more than people expect, especially on fast lines where there is little tolerance for movement.
Match the sealer head to the bottle and cap format
The sealer head must suit the container top area and the production speed. A head that is too large can waste energy and overheat the closure, while one that is too small may leave weak points at the edge of the foil. The correct head fit also depends on whether the bottle is round, square or a wider specialty shape. On some lines, the shoulder profile of the bottle influences how high the head should sit above the cap.
For setup, start with a test run at low speed. Check that the head is centred over the cap and that the bottle passes through without wobble. If the line has vibration from a worn conveyor or a loose guide rail, the cap may move and the seal line will shift. On coastal sites in Durban and Richards Bay, humidity can also affect cap handling and liner behaviour, so watch the line for any change after long shutdowns or weekend stoppages.
Use a step-by-step fitting check before production
Before you run a full batch, work through a short fitting check. This keeps downtime down and avoids wasting liners and product. It is a simple process but it saves a lot of trouble later, especially when operators are changing over between pack sizes.
- Confirm the bottle neck finish and cap specification from the approved sample.
- Inspect the liner type and make sure it matches the product, closure and shelf-life target.
- Set the sealer head height and centre point above the cap.
- Run 10 to 20 sample bottles and inspect the seal edge, lift test and closure fit.
- Record the settings for the next changeover and keep the approved sample with the line file.
If any of the samples show lifting, scorching or patchy bonding, stop and correct the setup. Do not just increase power and hope for the best. That can hide the fault for one shift and create bigger problems later.
Common signs that the cap size is not right
Most cap fit problems show up quickly once you know what to look for. A weak seal line, wrinkles in the foil or inconsistent pull-off strength can all point to a sizing issue. Sometimes the cap appears to close normally, but the liner is not making even contact. In other cases, the cap threads are correct but the neck ring or tamper band area is interfering with the seal cycle. It is a small detail, yet it can affect an entire production day.
- Caps feel loose or tighten unevenly by hand.
- The liner lifts on one side after cooling.
- Foil burns, darkens or shows an uneven imprint.
- Product leaks during transit or pallet movement.
- The tamper evidence ring does not sit cleanly after sealing.
If these symptoms appear after a packaging change, check the incoming bottle batch first. It is often the source of the fault, not the sealer itself.
Keep the fit stable across shifts, maintenance and supply changes
Once the cap and neck finish are matched, keep the setup stable. Preventive maintenance helps, but day-to-day control matters just as much. Train operators to spot minor differences in cap feed, bottle height and liner position. Keep spare parts, head settings and approved samples in one place so there is no guessing during load-shedding recovery or after a breakdown. A rushed restart often leads to misaligned sealing heads or mixed stock on the line.
For multi-site operations in Jacobs, Pinetown, Prospecton and Pietermaritzburg, keep the same measurement method at each plant. That makes it easier to compare results and support line commissioning or remote troubleshooting. If a supplier changes a cap mould or a bottle mould, update your records immediately. Good sealing depends on repeatable parts and clear records, not luck or guesswork.
When in doubt, test the full pack format, bottle, cap and liner together. A correct match gives you better shelf life, fewer call-backs and cleaner handling from filling through to dispatch.