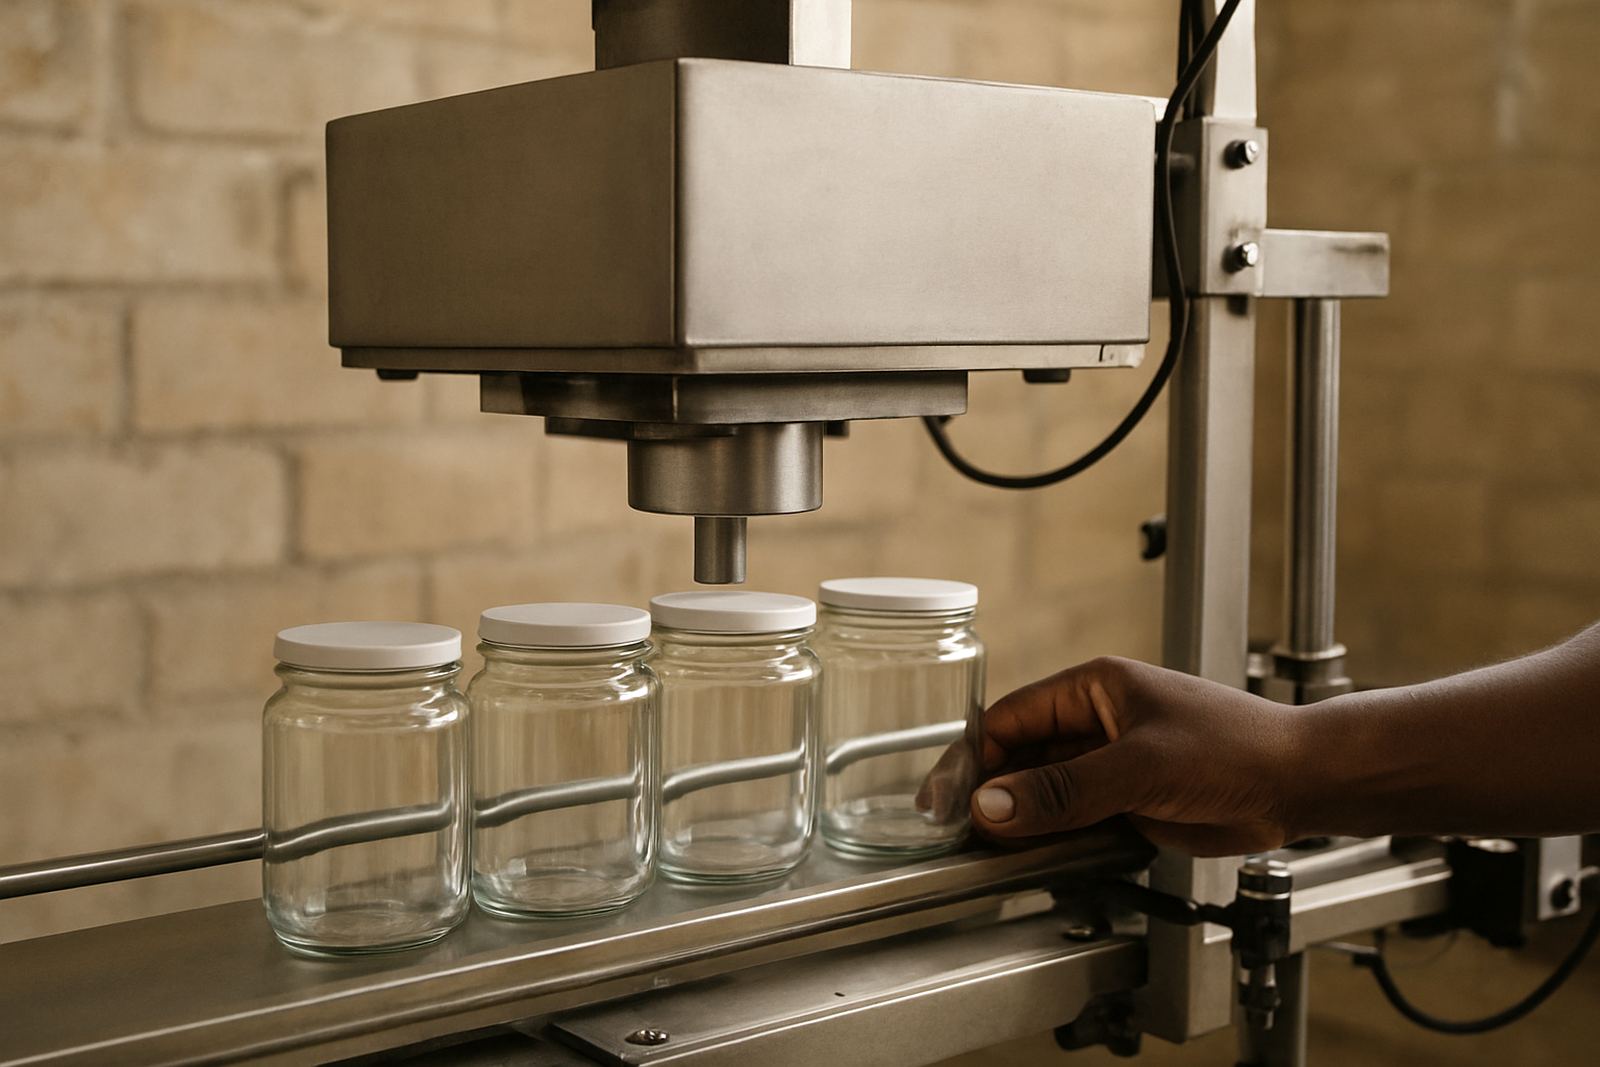
Why wide neck packs behave differently on the line
A wide neck container gives you more surface area to seal, but that does not make the job easier. With tubs and jars, the liner must cover a larger opening cleanly, sit flat, and heat evenly across the full mouth. If the neck finish is uneven, or the jar has a slight oval shape from mould wear, the seal can fail at the edges even when the centre looks fine.
In practice, the larger opening changes how the product moves under the capper and sealer. A thicker fill, a heavier container, or a softer plastic tub can all affect how well the seal lands. On a line in Jacobs or Prospecton, that often means checking the infeed guide, cap torque, and conveyor stability before touching the sealer settings. If the pack is wobbling, the seal is already at risk.
Wide neck sealing also responds more sharply to contamination. A small smear of sauce, powder, or moisture on the rim can create a leak path. That is why packers in food, pharma and chemical plants should treat rim cleanliness as part of the sealing system, not as a filling issue only.
Liner choice matters more on tubs and jars
For larger openings, liner matching is often the first point of failure or success. The liner needs the right diameter, thickness and heat response for the container material and the product inside. A liner that works well on a small bottle can bridge, curl, or seal weakly on a wide mouth jar.
Different products ask different things of the seal. Oily food products, powders, cleaning chemicals and tablets all transfer heat and pressure in their own way. In humid coastal conditions around Durban and Richards Bay, the packaging room can also affect the result. Condensation on cold packs, or damp cartons at changeover, can interfere with a clean bond.
- Check liner diameter against the true mouth opening, not just the nominal pack size.
- Match liner construction to the product, container material and storage conditions.
- Keep liners dry and sealed in storage, especially near the coast.
- Test for peel strength and leak resistance before running full production.
When the wrong liner is used, the fault is not always obvious at pack-off. The seal may hold during the shift, then fail in transport, warehousing or after a hot afternoon in a steel container yard. That is why proper liner matching should be part of commissioning, not an afterthought.
Heat settings need finer control than many teams expect
Wide neck induction sealing usually needs more care with heat distribution. Because the opening is larger, the energy must be spread more evenly across a wider area. If the output is too low, the edges stay weak. If it is too high, the liner can scorch, distort, or bond unevenly.
The right setting depends on line speed, container height, cap size, neck finish and the liner spec. A one-size-fits-all approach rarely holds up across a mixed pack list. Many South African plants run different sizes on one line, then wonder why the larger jar seal varies after a changeover. In most cases, the issue is not the sealer alone, but the full set-up around it.
- Confirm power stability if the plant is affected by load-shedding or generator switchover.
- Set the sealer to suit the fastest expected line speed, then verify at normal speed.
- Check cap torque after the first batch and again after warm-up.
- Record results for each container size so the next changeover is repeatable.
On a busy day in Pinetown or Pietermaritzburg, operators often adjust speed to chase output. That can be fine if the seal is still passing validation. If not, the team ends up packing product with a false sense of security. A small note on settings can save a lot of rework later, and yes it matters more than most people think.
What operators should watch during changeovers
Changeovers on wide neck lines need more than a quick cap swap. The pack geometry changes, the liner contact changes, and the product presentation may change too. If the team is moving from a narrow bottle to a wide jar, the operator should treat the first ten to twenty units as a test run.
Good operator training helps here because many seal defects show up as process clues before they become rejects. A slight cap tilt, a delayed feed, or a liner sitting off-centre can tell you the line is drifting. The sooner the operator spots it, the fewer packs are scrapped.
- Check the cap feed path for snagging on wider closures.
- Watch for product splash or fill levels too near the rim.
- Inspect the first seals for uniform bonding across the full circumference.
- Keep a sample jar from each shift for comparison if customer complaints arise.
In practice, plants in Jacobs and Prospecton often do well when they assign one person to watch the first part of the run after every changeover. That one habit cuts down on problems that otherwise only show up at dispatch or, worse, at the customer site.
Validation and preventive maintenance on wider openings
Seal validation on wide neck containers should reflect the actual use case, not only a lab result. If the product is likely to sit in a warm truck, move through coastal humidity, or spend time in a warehouse with dust and vibration, test for those conditions. The seal must hold after transport, stacking and handling, not just off the line.
Preventive maintenance also becomes more important because wide neck sealing can mask wear until it is quite advanced. Heating heads, guides, height adjustments and control settings need regular checking. If a component drifts out of position by even a few millimetres, the seal pattern may shift enough to weaken the bond.
For food and pharma packers, records matter. Keep validation notes by container size, liner type and product family. For chemical packs, include any safety or storage notes that affect the seal. This makes it easier to trace a fault and prove the corrective action was taken. It is basic good practice, but many teams only tighten up after the first complaint.
A Durban example for tubs, jars and real production pressure
A packing line in the Durban industrial area may run a morning batch of sauces, then switch to a dry powder or a chemical filler later in the day. That mixed schedule puts pressure on the seal setup because each product behaves differently. A wide neck tub with a wet fill needs a different handling approach from a jar filled with a dry blend.
When a team tries to force the same settings across all pack types, problems usually show up as slow leaks, cap distortion, or intermittent failure. The smarter approach is to document settings by pack format, then confirm them during commissioning and again after any service work. If a line is being moved, expanded or repaired, the wide neck settings should be rechecked from scratch.
That is where on-site support, remote support and spares planning all help. A plant does not just need a machine that turns on. It needs the right liner, the right height, the right speed and the right service response when the line starts acting up. For businesses running across Jacobs, Pinetown, Richards Bay and beyond, that practical support can keep stock moving without guessing at the cause.
Wide neck sealing is not difficult, but it is less forgiving than many teams expect. Once the opening gets bigger, every small choice counts a bit more, and that is exactly why the process deserves proper attention.